Natural Vitamin E Acetate Powder 700 IU CWD
Our Natural Vitamin E Acetate Powder 700 IU CWD features premium, plant-derived d-alpha tocopheryl acetate. Specially engineered for high-end dietary supplements and functional beverages, this standardized granulated powder overcomes traditional oily blending barriers to deliver superior chemical stability, cold water dispersibility, and processing flexibility.
Why Choose Our Natural Vitamin E CWD Powder?
• 100% Plant-Derived: Pure d-alpha tocopheryl acetate from non-GMO vegetable oils, delivering up to 2× the bioavailability of synthetic vitamin E.
• Cold Water Dispersible (CWD): Disperses instantly and uniformly in cold liquids without oil slicking, phase separation, or clumping, making it ideal for functional beverages and water-based formulations.
• Acetate Ester Protection: The vitamin E acetate ester structure provides enhanced resistance to heat, light, and industrial shear forces, supporting improved stability during processing and storage.
• Streamlined Processing: Free-flowing, non-dusting vitamin E powder optimized for high-speed tableting, capsule filling, and premium premixes.
Custom Vitamin E Formulation Solutions
Backed by our advanced formulation delivery platform—including Liposomal Technology, Pellet Technology, and Microencapsulation Technology—we offer tailored vitamin E potencies, customized carriers, and professional OEM/contract manufacturing services.
Contact us today to request a sample, discuss your vitamin E formulation requirements, and optimize your dietary supplement, functional beverage, or nutraceutical formulation.
Description
Our Natural Vitamin E Acetate Powder 700 IU CWD is a highly stable, premium-grade nutritional ingredient featuring bioavailable d-alpha tocopheryl acetate derived from non-GMO vegetable oils. Engineered utilizing proprietary Advanced Microencapsulation Technology, this standardized free-flowing powder overcomes the inherent formulation constraints of traditional oily Vitamin E. It delivers exceptional stability, superior mixing homogeneity, and seamless cold water dispersibility, providing a turnkey solution for modern dietary supplements, functional beverages, and fortified food formulations.
Product Specifications & Technical Overview
Product Name:Natural Vitamin E Acetate Powder 700 IU CWD
Active Ingredient:Natural Vitamin E (d-Alpha Tocopheryl Acetate)
Chemical Form:Acetate Ester (Enhanced Stability Structure)
Active Potency:Standardized Minimum 700 IU/g (d-alpha tocopherol equivalent)
Solubility Grade:CWD (Cold Water Dispersible)
Production Source:Non-GMO Plant-Derived / Vegetable Oils
Encapsulation Carrier:Food-grade modified starch and customized carbohydrate matrix
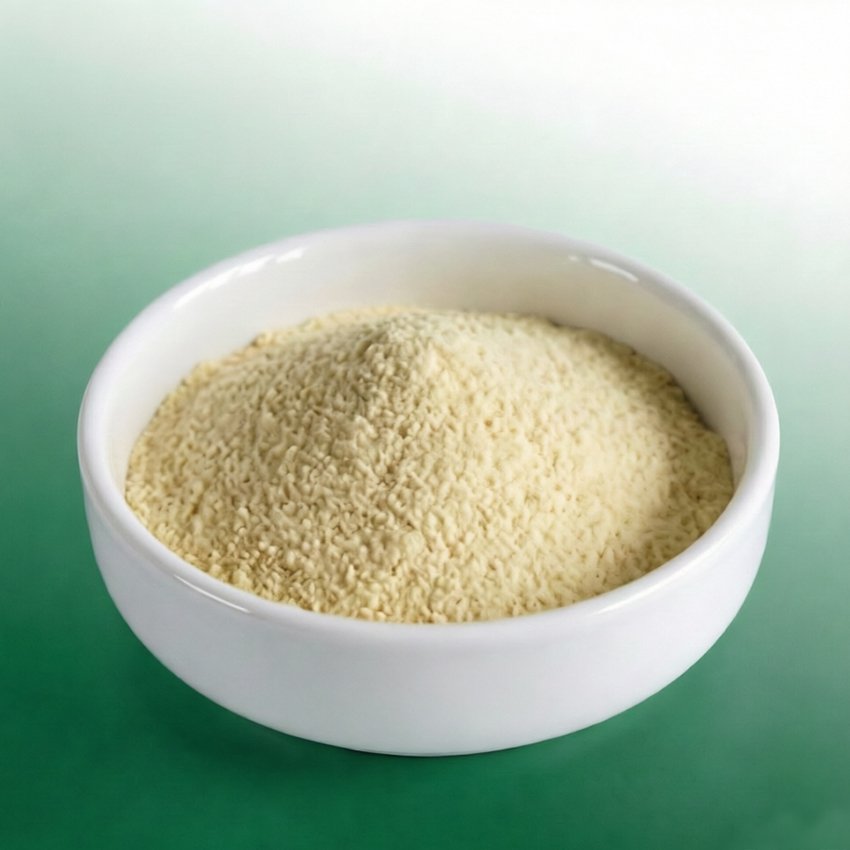
Physical Appearance:Off-white to light yellow, free-flowing granulated powder
Primary Applications:Dietary supplements, functional foods, nutritional powders, beverages, and premixes
1.Advanced Technical Characteristics & Science
1.1 100% Plant-Derived d-Alpha Tocopheryl Acetate
The active core of this ingredient consists entirely of natural d-alpha tocopheryl acetate, sourced from sustainable, non-GMO botanical oils. Unlike synthetic Vitamin E (dl-alpha-tocopherol), the natural d-isomer possesses a specific molecular stereochemistry that perfectly aligns with human cellular transport proteins. This structural alignment delivers up to 2x higher biological activity and cellular retention compared to synthetic alternatives. B2B manufacturers can confidently leverage this clear-cut clinical superiority to satisfy clean-label consumer demands.
1.2 Acetate Esterification for Superior Shelf-Life
Unesterified natural tocopherol is highly prone to oxidation when exposed to atmospheric oxygen, processing heat, and UV light, which rapidly leads to potency loss and rancidity. By transforming natural tocopherol into its acetate ester form (d-alpha tocopheryl acetate), we lock the active antioxidant center. This molecular modification ensures that the raw material exhibits extreme resilience against processing stresses and guarantees long-term label claim survival in finished product packaging.
1.3 Advanced Microencapsulation Barrier
To bridge the gap between oil-based nutrients and powder processing, we utilize proprietary Microencapsulation Technology. Each micro-droplet of natural Vitamin E oil is fully embedded within an engineered, oxygen-impermeable carbohydrate matrix. This specialized shell acts as a physical shield, preventing structural degradation, eliminating cross-ingredient cross-linking in complex formulations, masking natural organic off-notes, and optimizing industrial flowability.
1.4 Flawless Cold Water Dispersible (CWD) Performance
Traditional Vitamin E acetate is a viscous, hydrophobic oil that cannot dissolve or disperse in water-based systems without heavy emulsifiers, leading to phase separation and oily rings. Our specialized CWD grade modifies the surface energy of the micro-capsules. When added to cold water or room-temperature liquids, the granulated powder wets instantaneously and disperses uniformly. It forms a stable, milky, homogeneous suspension without precipitation, floating spots, or residue.
2.Why Partner with Us? (B2B Processing Advantages)
Selecting the right raw material supplier determines the processing efficiency of your production line. Our Natural Vitamin E 700 IU CWD Powder provides clear manufacturing advantages:
- Excellent Mechanical Stability:The reinforced microcapsules withstand heavy shear forces during industrial ribbon blending and high-speed tableting compression without leaking core oils.
- Precision Homogeneity in Premixes:Standardized at 700 IU/g, the particle size distribution is strictly controlled to match common mineral and vitamin carriers, preventing ingredient segregation during transit.
- Zero Static & Free-Flowing:The non-dusting granulated powder eliminates static cling, prevents automatic hopper clogging, speeds up plant cleanup, and minimizes weight variation during high-speed encapsulation.
- Turnkey Customization & OEM:We provide tailor-made potencies, customized wall matrices, and application-specific particle size modifications to match your operational equipment.
3.Targeted Nutritional Applications
3.1Premium Dietary Supplements
Optimized for high-speed tableting, hard-shell vege-capsule filling, single-serve stick packs, and two-piece gelatin systems. Its exceptional flowability ensures precise volumetric dosing across massive production batches.
3.2Functional Powders & Dry Beverage Mixes
The ultimate choice for meal replacements, instant protein powders, collagen peptide blends, and sports nutrition pre-workout mixes. The CWD properties ensure complete, lump-free reconstitution by the end consumer in seconds.
3.3Liquid Formulations & Fortified Beverages
Perfect for ready-to-drink (RTD) functional juices, fortified dairy drinks, plant-based milks, and liquid vitamin drops. The micro-capsules keep the hydrophobic core oil suspended evenly throughout the liquid matrix, preventing phase separation.
3.4High-Potency Vitamin & Mineral Premixes
Industrial premix blenders utilize our 700 IU powder to secure reliable uniformity in complex, multi-ingredient blends, safeguarding chemical stability until end-user consumption.
4.Advanced Formulation Technology Platform
Our technical expertise extends beyond standard encapsulation. We operate a multi-disciplinary ingredient delivery platform designed to resolve complex solubility and bio-absorption bottlenecks across diverse active compounds (lipids, carotenoids, amino acids, and botanicals):
- Liposomal Delivery Technology:Multi-layer lipid vesicles that bypass harsh gastric environments for optimized cellular uptake.
- Pellet & Granulation Engineering:Delivers targeted, time-release profiles and controls bulk density for high-end capsule systems.
- Submicroencapsulation Solutions:Sub-micron structures engineered for crystal-clear optical transparency in liquid delivery systems.
- Cocrystal & Co-amorphous Frameworks:Rearranges molecular crystal structures to amplify the dissolution velocity of poorly soluble compounds.
Our international technical support team stands ready to audit your formula, resolve matrix compatibility issues, and deliver optimized ingredient modifications.
5.Regulatory Compliance & Documentation
Every commercial batch is backed by a fully auditable paper trail, ensuring seamless regulatory clearance with global compliance agencies (FDA, EFSA, TGA, etc.):
- Certificate of Analysis (COA) & Comprehensive Batch Manufacturing Records
- Material Safety Data Sheets (MSDS/SDS)
- 100% Allergen-Free Statements
- Plant-Derived / Vegan Compliance Certification
- Authorized Kosher and Halal Documentation
FAQ
Q1: What does “700 IU” represent in this Natural Vitamin E powder?
A: IU stands for International Unit, which measures biological efficacy rather than simple mass. A concentration of 700 IU/g means that every single gram of our microencapsulated powder delivers 700 International Units of active d-alpha tocopherol equivalence. This high-potency standardization allows manufacturers to achieve maximum nutritional values using low inclusion weights, leaving ample room in formulas for other active ingredients.
Q2: What is the biological advantage of natural d-alpha over synthetic Vitamin E?
A: Synthetic Vitamin E (dl-alpha-tocopherol) is a chemical mixture of eight different stereoisomers, only one of which perfectly matches the human body. Our natural d-alpha tocopheryl acetate is a single, pure isomer. Human liver transport proteins selectively recognize and utilize the “d” form, resulting in significantly higher bioavailability, longer plasma half-life, and superior tissue retention compared to synthetic versions.
Q3: Why choose the “Acetate” form instead of pure d-alpha tocopherol?
A: Pure d-alpha tocopherol is a highly sensitive free radical scavenger that oxidizes quickly upon contact with air, causing it to degrade during manufacturing storage. The acetate form chemically protects this sensitive hydroxyl group. Once consumed, human intestinal esterase enzymes naturally break the acetate bond, releasing the fully active, pure natural Vitamin E into the bloodstream. It balances maximum industrial shelf life with optimal biological efficacy.
Q4: How does “Cold Water Dispersible (CWD)” differ from true water solubility?
A: Because natural Vitamin E is an oil, it can never be truly soluble in water at a molecular level without chemical modification. Our CWD technology uses food-grade hydrophilic amphiphilic carriers to trap micro-droplets of the oil. When exposed to cold liquids, these carriers instantly wet and release a stable, microscopic suspension throughout the water. This achieves the visual and functional properties of a soluble powder without breaking down the natural vitamin structure.
Q5: Is this ingredient compatible with automated capsule and tablet machinery?
A: Yes. Untreated Vitamin E oil cannot be put into powder machinery. Our advanced microencapsulation transforms the sticky liquid oil into an off-white, free-flowing granulated powder. It possesses a tailored tap density and an optimized angle of repose, minimizing machine friction, eliminating static build-up, and ensuring seamless operation on high-speed industrial presses.


Reviews
There are no reviews yet.