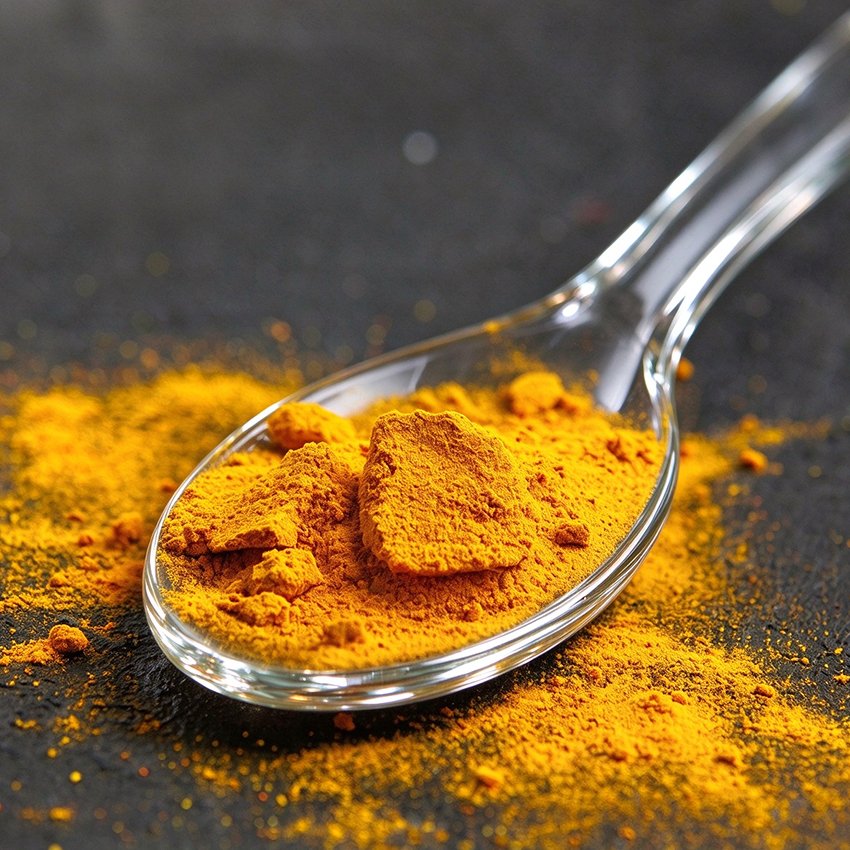
Berberine Granulation Powder Granulated Berberine for Tablets, Capsules and Nutritional Formulations
Berberine Granulation Supplier Granulated Berberine
Berberine Granulation Powder Granulated Berberine for Tablets, Capsules and Nutritional Formulations
Berberine Granulation is a specialized granulation solution for Berberine, a naturally occurring botanical alkaloid commonly obtained from plants such as Coptis chinensis and Berberis species. Berberine is widely used as an active ingredient in dietary supplements, botanical formulations, functional nutrition products and other nutritional ingredient applications.
In conventional Berberine powder form, the ingredient may present processing challenges, including limited powder flowability, particle segregation, dust generation and difficulties with consistent material feeding and filling. These characteristics can affect manufacturing efficiency in tablet compression, capsule filling and other solid dosage applications.
Berberine Granules are developed using specialized Granulation Technology, which processes Berberine powder together with selected formulation components into granular materials with controlled particle size and physical characteristics. Compared with conventional Berberine powder, the granulated format can provide improved flowability, reduced powder segregation and more consistent material handling, supporting downstream manufacturing processes.
Depending on the formulation requirements, Berberine can be processed through Wet Granulation or Dry Granulation. Wet Granulation involves controlled mixing, binder addition, granulation, drying and particle sizing, while Dry Granulation uses mechanical compaction followed by milling and particle-size classification. The appropriate granulation method depends on the ingredient properties, formulation composition, target granule characteristics and manufacturing requirements.
Granulation Technology is widely used across pharmaceuticals, chemicals, food, dietary supplements, sports nutrition, agriculture and animal nutrition. Its primary purpose is to improve the physical properties of powder materials to better meet requirements for downstream processing, storage, transportation and final product manufacturing.
Berberine is just one example of our custom granulation capabilities. We provide custom granulation services for a wide range of active ingredients, with specifications tailored to the customer’s target active content, particle size, granule characteristics, dosage form and manufacturing requirements. Our customized ingredient processing solutions are designed for dietary supplement manufacturers, nutraceutical brands, botanical ingredient suppliers, raw material distributors and OEM/ODM manufacturers seeking granulated ingredients for commercial production.
Description
1.What Is Berberine Granulation?
Berberine Granulation is a granulated form of Berberine produced using controlled Granulation Technology.
The process converts conventional powder into granular material with defined physical characteristics, making the ingredient more suitable for downstream processes such as tablet compression, capsule filling and sachet filling.
Granulation can also be customized according to the characteristics of different active ingredients and their intended applications.
2.What Is Granulation Technology?
Granulation Technology is a processing technology that converts materials in different physical states, including powders, melts and solutions, into granular products with defined shapes and particle-size characteristics through specific processing procedures.
The core purpose of granulation is to improve the physical properties of materials so they can better meet the requirements of subsequent processing or final use.
Granulation Technology is widely applied in:
- Pharmaceuticals
- Dietary Supplements
- Food & Functional Foods
- Sports Nutrition
- Chemical Industry
- Agriculture
- Animal Nutrition & Feed
- Nutritional Products
- Tablet Manufacturing
- Capsule Manufacturing
- Other Powder Processing Applications
This broad application range makes Granulation Technology a versatile solution for companies that need to convert conventional powders into more manageable and process-friendly granular materials.
3.Berberine Granulation Process
3.1Wet Granulation
A typical Wet Granulation process includes:
Raw Material Pretreatment → Dry Mixing → Binder Addition & Wet Mixing → Granulation → Drying → Sizing → Finished Granules
Berberine is mixed with selected formulation components before a suitable binder system is introduced. The material is then processed into granules, dried and sized according to the required particle characteristics.
Wet Granulation can be considered when improved binding, flowability or compression characteristics are required.
3.2Dry Granulation
Dry Granulation uses mechanical compaction without a conventional wetting and drying process.
Typical process:
Powder Material → Screw Feeding → Roller Compaction → Compact Sheet Formation → Milling & Sizing → Qualified Granules
Key processing parameters can include:
- Screw feeding speed
- Roller speed
- Compaction pressure
- Granulation or milling speed
- Particle-size control
Dry Granulation can be considered when a low-moisture processing route is preferred.
4.Why Granulate Berberine?
4.1Improved Flowability
Granulated Berberine can provide improved flow characteristics compared with fine powder, supporting more stable feeding and filling during production.
4.2Reduced Powder Segregation
Granulation can help reduce segregation between Berberine and other formulation components, supporting more consistent material distribution.
4.3Better Tablet Compression
The granular structure can provide improved material feeding characteristics during tablet compression and support more consistent tablet production when the formulation is properly designed.
4.4Improved Capsule Filling
Granulated Berberine can provide more controlled filling characteristics and reduce issues associated with fine powder segregation.
4.5Reduced Dust Generation
Compared with fine powder, granular material can help reduce dust during handling, conveying and production.
4.6Improved Direct Oral Characteristics
For products intended for direct consumption, granulation can improve physical handling and mouthfeel. Sweeteners, flavors or other formulation components can be incorporated during granulation where appropriate.
5.Berberine Granulation vs. Conventional Powder
| Property | Conventional Berberine Powder | Berberine Granulation |
| Flowability | May be limited | Improved |
| Powder Segregation | More likely | Reduced |
| Tablet Compression | May require additional formulation adjustment | More suitable |
| Capsule Filling | Can be affected by powder flow | Improved handling |
| Dust Generation | Relatively higher | Reduced |
| Dosage Consistency | Can be affected by segregation | More consistent physical distribution |
| Direct Oral Use | Powder texture may be less convenient | Granulated format can improve handling |
| Storage & Transportation | More dependent on powder handling conditions | Improved physical handling characteristics |
6.Core Advantages of Granulation Technology
6.1 Tablet Compression
Granules generally exhibit better flowability than conventional powders, helping improve material feeding and supporting more consistent tablet production.
6.2 Capsule Filling
Granulated materials can support more controlled filling and reduce segregation between different formulation components.
6.3 Direct Oral Ingestion
Granulation can improve the physical characteristics and mouthfeel of products intended for direct consumption. Sweeteners or flavoring components can be incorporated during granulation where appropriate.
6.4Storage & Transportation
Granulated materials can provide improved handling characteristics and may help reduce powder dusting, segregation and caking, depending on the formulation and packaging conditions.
7.Customized Granulation for Multiple Active Ingredients
Berberine is only one example of our Granulation Technology capabilities.
We can develop and customize granulated products for a wide range of active ingredients according to the customer’s formulation and manufacturing requirements.
Potential customization includes:
- Active ingredient content
- Granulation formulation
- Wet Granulation or Dry Granulation
- Particle size
- Particle-size distribution
- Binder and excipient system
- Bulk density
- Flowability requirements
- Tablet compression requirements
- Capsule filling requirements
- Direct oral formulation requirements
- Packaging format
Our granulation solutions can be considered for botanical extracts, vitamins, amino acids, minerals, nutritional ingredients and other active compounds where improved powder processing characteristics are required.
If you have an active ingredient that is difficult to handle as a conventional powder, you can provide us with the ingredient name, target content, particle-size requirement and final dosage form, and we can evaluate a suitable granulation approach.
8.Granulation Technology Across Different Industries
Our Granulation Technology is not limited to botanical or nutritional ingredients. It can be applied to different material systems according to their physical characteristics and final applications.
8.1Pharmaceutical Industry
Granulation is widely used to improve the processing characteristics of pharmaceutical powders for tablet compression and capsule filling.
8.2Food Industry
Granulation can improve the handling, flowability and dosage characteristics of food ingredients and functional food materials.
8.3Dietary Supplements
Vitamins, minerals, botanical extracts, amino acids and other active ingredients can be granulated for tablets, capsules, sachets and direct-consumption products.
8.4Sports Nutrition
Granulation can be applied to amino acids, nutritional compounds and other sports nutrition ingredients requiring improved powder handling.
8.5Chemical Industry
Powdered chemical materials can be processed into granules with controlled particle size and improved handling characteristics.
8.6Agriculture
Granulation can be used for agricultural ingredients and formulations where controlled particle size and improved physical properties are required.
8.7Animal Nutrition & Feed
Granulation can also be considered for nutritional ingredients and feed-related materials requiring improved handling, mixing and processing characteristics.
This broad application range allows us to provide customized Granulation Technology solutions for different industries and a wide range of active ingredients.
9.Active Ingredient Processing & Delivery Technology
Our active ingredient technology platform includes several distinct processing routes:
9.1Granulation Technology
Converts powders or other materials into granules with controlled physical characteristics, improved flowability and better downstream processing performance. Suitable for tablets, capsules, sachets, nutritional powders and other solid formulations.
9.2Pellet Technology
Produces small spherical or near-spherical pellets with a controlled multi-unit structure. Pellet Technology is a separate technology from conventional granulation and is suitable for applications requiring a defined pellet format.
9.3Liposomal Technology
Uses phospholipid-based carrier systems to develop liposomal formulations for active ingredients requiring a specialized delivery format, particularly for liquid and dispersion-based applications.
These technologies are selected according to the characteristics of the active ingredient, target dosage form and customer’s formulation requirements.
10.Berberine Content & Customization
Berberine Granulation can be customized according to the customer’s formulation and production requirements.
Customization may include:
- Berberine content
- Granulation formulation
- Wet or Dry Granulation
- Particle size
- Particle-size distribution
- Binder and excipient system
- Bulk density
- Flowability
- Tablet compression characteristics
- Capsule filling characteristics
- Packaging format
The final specification can be discussed according to the customer’s target dosage form, production equipment and formulation requirements.
11.Applications
11.1Dietary Supplements
Suitable for Berberine-based nutritional supplements in tablet, capsule, sachet and powder formats.
11.2Botanical & Herbal Formulations
Suitable for botanical formulations using Berberine as an active ingredient.
11.3Tablets
Granulated Berberine can provide improved feeding and flow characteristics for tablet compression.
11.4Hard Capsules
The granular format can support more consistent filling and reduce segregation during capsule production.
11.5Powder Sachets
Suitable for single-dose nutritional powders and ready-to-mix formulations.
11.6Direct Oral Products
Granulated Berberine can be incorporated into direct-consumption products, with formulation adjustments available for mouthfeel and flavor requirements.
11.7Functional Foods
Can be considered for functional food and nutritional formulations depending on the final product design.
Supply & Customization
We provide Berberine Granulation as part of our broader customized Granulation Technology service.
In addition to Berberine, we can develop granulated products for multiple active ingredients, including botanical extracts, vitamins, amino acids, minerals and other nutritional or functional ingredients.
Both Wet Granulation and Dry Granulation can be considered according to the characteristics of the material and the customer’s final application.
We can support customized requirements including active ingredient content, formulation composition, particle size, physical characteristics, dosage form and packaging.
Our production system operates under FSSC 22000, ISO 22000 and HACCP management systems.
Samples and technical documents can be provided for formulation evaluation and customer testing.
FAQ
1.What is Berberine Granulation?
Berberine Granulation is Berberine processed through Granulation Technology to convert conventional powder into granular material with improved physical and processing characteristics.
2.Why use Granulated Berberine instead of conventional powder?
Granulation can improve flowability, reduce powder segregation and dust, and make Berberine more suitable for tablet compression, capsule filling and other downstream processes.
3.Can Berberine Granulation be used for tablets?
Yes. Granulated Berberine is suitable for tablet compression and can be adjusted according to the customer’s production requirements.
4.Can it be used for capsules?
Yes. Granulated Berberine can be used for hard capsule filling and can provide improved handling compared with conventional fine powder.
5.Do you provide Wet Granulation and Dry Granulation?
Yes. The appropriate granulation route can be selected according to the material characteristics and final application.
6.Can the particle size be customized?
Yes. Particle size and particle-size distribution can be adjusted according to the customer’s formulation and equipment requirements.
7.Can other ingredients be added during granulation?
Yes. Excipients, binders, sweeteners and other formulation components can be considered depending on the target product and processing route.
8.Can you granulate other active ingredients besides Berberine?
Yes. Berberine is only one example. We can develop customized Granulation Technology solutions for various botanical extracts, vitamins, amino acids, minerals and other active ingredients.
9.What information should I provide for a customized granulation project?
The ingredient name, target active content, preferred dosage form, particle-size requirement and intended application are helpful starting points for evaluating a suitable granulation process.
10.Is Granulation Technology only used for nutritional ingredients?
No. Granulation Technology is widely used in pharmaceuticals, food, dietary supplements, sports nutrition, chemical products, agriculture, animal nutrition and other industries.
11.Can you provide samples?
Yes. Samples and technical documents can be provided for formulation evaluation and customer testing.


Reviews
There are no reviews yet.